Precision-manufactured machinery and industrial storage modules engineered to interface directly with automated roller conveyor topologies, dynamic buffering zones, and vertical lifting transfer nodes.
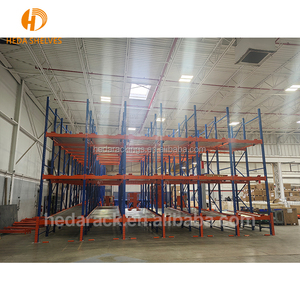
Full-lane gravity rollers with integrated centrifugal speed controller brakes for high-throughput FIFO buffer staging.
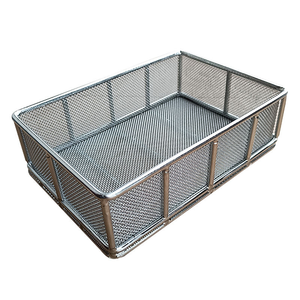
Electro-polished SUS304 wire cages designed for automated ultrasonic parts wash, drain conveyance, and robotic picking lines.
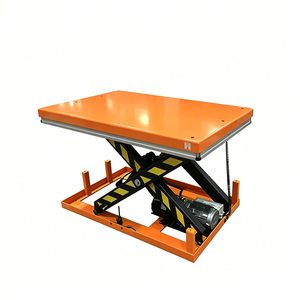
Heavy-duty 3-ton electro-hydraulic lifting node outfitted with optional powered roller deck for line height synchronization.
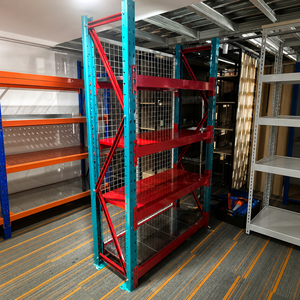
Roll-formed high-tensile steel frames designed to host conveyor feeds, pick-tunnels, and automated pallet live-storage bays.
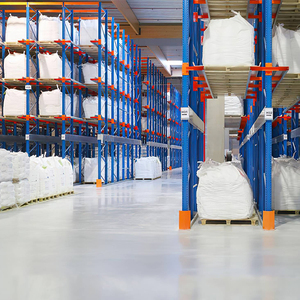
High-density channel storage customized with floor guide rails or roller-bed shuttles to maximize cubic warehouse yield.
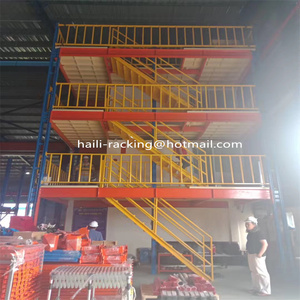
Engineered multi-level structural steel platforms engineered to support continuous roller conveyor runs and vertical spiral sorters.
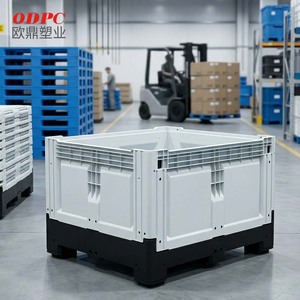
Reinforced flat-runner HDPE base optimized for smooth travel across chain driven and motorized roller conveyor beds.
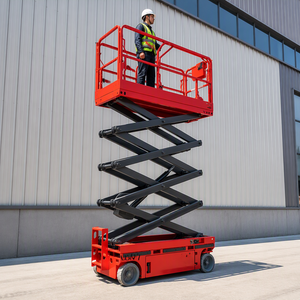
Manned access equipment essential for the safe mechanical erection, overhead sensor wiring, and routine inspection of elevated conveyor spans.
Modern distribution facilities, automotive assembly plants, and automated e-commerce fulfilment hubs demand material handling solutions that transcend off-the-shelf catalog parameters. As a tier-1 OEM and ODM manufacturer of industrial roller conveyor systems, our factory delivers customized intralogistics architectures designed to eliminate process bottlenecks, enhance payload ergonomics, and minimize cumulative mechanical wear under continuous operational duty.
Roller conveyor systems represent the structural backbone of horizontal and low-gradient vertical transport within facilities. Whether moving delicate 200-gram pharmaceutical totes or rugged 2,500-kilogram industrial engine blocks, conveyor efficiency hinges directly upon roller tube concentricity, dynamic balance, bearing seal integrity, and drive transmission engineering. By operating our own metallurgical processing, precision tube extrusion, and robotic welding lines, our engineering group controls each fabrication variable to satisfy tight international tolerances (ISO 9001:2015, CE machinery directives, and ANSI/CEMA standards).
Full OEM flexibility covering bespoke roller diameters (ø38mm, ø50mm, ø60mm, ø76mm, ø89mm), center-to-center roller pitches, between-frame widths (BF 200mm to 1800mm), and heavy-gauge galvanized or powder-coated channel side-frames.
Engineered integration of Motorized Driven Roller (MDR 24V/48V BLDC) intelligent zones, Poly-V serpentine high-speed belt loops, O-ring elastomeric bands, tangentially driven sprockets, and rugged duplex roller chain linkages.
Engineered material variants including carbon steel with yellow zinc dichromate passivation, electro-polished AISI 304/316 stainless steel for food and washdown sanitary zones, PVC rollers for sensitive parcel handling, and polyurethane-lagged anti-slip sleeves.
Drawing on an 18-year industrial engineering lineage grounded in turnkey warehouse logistics across the UAE and GCC, our team pairs structural storage knowledge with active continuous conveyor engineering. This symbiotic design philosophy guarantees that conveyor transfers seamlessly feed into selective pallet racks, heavy-duty flow racks, mezzanine platforms, and automated pick modules without physical alignment tolerances drifting during multi-shift operations.
Choosing an intralogistics manufacturing partner requires assessing beyond basic brochure claims. Procurement officers and chief supply chain engineers require guaranteed structural repeatability, comprehensive traceability, and deep domain experience. Here is how our production facilities and service operations safeguard your project investments:
Since our inception in 2005, our engineering core has executed over 500 extensive industrial material handling and storage installations. From high-capacity distribution centers in Sharjah, Dubai, and Abu Dhabi to complex multi-tier mezzanine picking facilities across international logistics hubs, our seasoned project managers navigate structural constraints, floor slab load variations, and aggressive timelines with zero project failures.
Unique in the intralogistics machinery manufacturing sector, our clients receive access to our proprietary cloud-based Real-Time Project Tracking System. This platform enables procurement teams and project engineers to monitor milestoned progress 24/7—tracking raw steel batch testing, robotic laser tube cutting, roller spin-balancing, powder-coating cure ovens, pre-shipment FAT tests, and live port customs clearance with zero guesswork.
We eliminate multi-contractor friction. A single accountable enterprise covers the complete lifecycle: on-site laser floor surveys, 3D CAD/BIM collision modelling, finite element analysis (FEA) under dynamic load stresses, domestic/export logistics, in-house mechanical & electrical erection, and annual compliance load safety inspections.
Our OEM/ODM conveyors are not merely mechanical metalwork; they are smart automated conduits. We engineer pre-wired electrical quick-disconnect harnesses and program intelligent IO-Link, AS-Interface, PROFINET, or EtherNet/IP distributed bus modules to ensure frictionless handshake with customer Warehouse Management Systems (WMS).
Selecting the optimal roller conveyor system requires matching payload characteristics (dimensions, bottom profile, rigidity, mass distribution) against operational velocity, indexing frequencies, and ambient operational conditions. Below is an engineering evaluation matrix of primary roller conveyor architectures manufactured by our OEM/ODM facility:
| System Architecture | Drive Transmission | Unit Payload Range | Ideal Operational Domain | Key Engineering Highlights |
|---|---|---|---|---|
| MDR (Motorized Driven Roller) | Brushless DC (24V/48V) inside roller tube via Poly-V belts | 0.5 kg – 75 kg (Cartons / Totes) | High-velocity e-commerce sorting, parcel hubs, pharmaceuticals | True Zero Pressure Accumulation (ZPA), energy-on-demand zones, ultra-low decibel (<58 dBA). |
| CDLR (Chain Driven Live Roller) | Continuous single or roll-to-roll roller chains with forged steel sprockets | 200 kg – 3,500 kg (Full Pallets / Drums) | Heavy manufacturing, palletizing lines, automotive casting plants | Positive slip-free drive torque, grease-packed welded sprockets, resistant to oil, dust, and foundry heat. |
| Lineshaft Powered Conveyor | Continuous rotating steel line shaft coupled with elastomeric drive belts | 1 kg – 40 kg (Medium Packages) | Cost-sensitive distribution centers, light assembly lines | Economical long runs powered by a single geared drive motor, low-maintenance mechanical slip-clutch action. |
| Gravity Roller & Flow Tracks | Unpowered gravity incline (1.5°–4.5°) or manual push conveyance | 5 kg – 1,500 kg (Cartons & Pallets) | FIFO order replenishment, trailer loading/unloading, pick tunnels | No electrical consumption, zero cabling, equipped with internal centrifugal brake rollers to control speed. |
| Belt-Driven Live Roller (BDLR) | Flat return belt pressed against roller underside via snubber rollers | 2 kg – 100 kg (Irregular Bottoms) | Airport baggage sorting, corrugated container processing plants | High-traction continuous linear speeds up to 120 m/min, exceptional tracking under high-friction cargo. |
1. Rigid Polypropylene Totes & Corrugated Boxes: For standardized container movements, we advise specifying our ø50mm MDR Zero-Pressure Accumulation Systems. Utilizing high-efficiency 24V or 48V brushless DC inner-motor rollers linked with 9-rib Poly-V belts, each 600mm to 900mm zone operates independently. Optical retro-reflective retro-sensors detect tote entry and cut power instantly when downstream accumulation is sensed, reducing warehouse baseline electrical consumption by upwards of 60% compared to continuously running legacy conveyors.
2. Wood Pallets, Wire Baskets & Collapsible Bulk Crates: Transporting heavy industrial containers—such as our Heavy Duty Industrial Collapsible Bulk Containers or steel pallet bases—mandates ø76mm or ø89mm Structural CDLR Systems. Bottom runners on wooden pallets often exhibit warping, nails, or rough grain. A chain-driven live roller creates positive, unyielding traction that pushes through irregular surfaces where belt friction drives would slip and burn.
3. Heavy-Duty Buffer Bays & Mezzanine Feed Lines: Where roller conveyors converge into high-density structural racking, such as our FIFO Gravity Pallet Flow Racking Systems or feed directly across a Modular Mezzanine Floor, we engineer mechanical entry funnel guides, heavy-gauge steel side drop barriers, and pneumatic roller stops to guarantee that loads are square prior to entry into structural racking channels.
Global supply chain disruptions, soaring industrial energy costs, and the rapid adoption of autonomous mobile robots (AMRs) have fundamentally restructured intralogistics procurement protocols. Supply chain executives and capital procurement directors no longer evaluate conveyors solely on raw meter-run capital expenditure (CapEx). Instead, forward-looking procurement methodologies prioritize the following long-term strategic benchmarks:
Procurement teams are phasing out oversized 3-phase AC continuous central motors in favor of decentralized 24V and 48V Brushless DC Motorized Driven Rollers (MDR). By transitioning to localized "Run-on-Demand" micro-zones, enterprises achieve immediate Scope 2 greenhouse gas emissions reductions and qualify for green industrial facility certifications (LEED / Estidama).
Fixed, single-purpose conveyor routings are obsolete. Modern procurement directives favor standard bolt-together aluminum and roll-formed steel side-frames that can be lengthened, re-routed, divided, or integrated with diverters and vertical lifts over a weekend without requiring hot structural metal welding.
Bypassing regional distributors and trading brokers to partner directly with an established engineering manufacturer reduces project capital expenditure by 25% to 40%. Direct factory partnership also provides open-source CAD data, custom gear ratio adaptations, and immediate access to original mechanical replacement parts without long distributor delays.
Furthermore, procurement evaluation guidelines now systematically scrutinize supplier total life-cycle cost (TCO). A conveyor roller equipped with precision ground chrome-steel ball bearings (ABEC-1 or ABEC-3) packed with synthetic low-friction lithium grease yields a Mean Time Between Failures (MTBF) exceeding 60,000 continuous hours—drastically reducing scheduled operational maintenance budgets compared to cheap commercial-grade unground carbon bearings.
As the Fourth Industrial Revolution (Industry 4.0) permeates modern material handling, roller conveyors are transforming into intelligent, cyber-connected industrial endpoints. Our research and development department focuses on several core technological development vectors that define next-generation automated material handling:
The standard motorized roller is evolving into a smart edge device. Our latest generation of OEM ODM motorized conveyor rollers can be outfitted with embedded micro-sensors that measure real-time internal core motor temperature, bearing vibration signatures (via 3-axis MEMS accelerometers), and cumulative mechanical rev-counts. By transmitting telemetry via IO-Link gateways to the facility's SCADA or maintenance dashboard, the system predicts bearing spalling or gearhead fatigue weeks before a physical breakdown occurs, eliminating catastrophic unscheduled line stoppages.
Autonomous Mobile Robots (AMRs) and Automated Guided Vehicles (AGVs) are ubiquitous in modern facilities. However, AMRs cannot replace fixed high-volume linear throughput conveyors. The cutting edge of intralogistics lies at the intersection of both technologies: docking conveyor transfer stations. We design custom motorized roller spur nodes equipped with precise optical communication interlocks (Optical ECI), allowing mobile robots to dock with millimeter precision, trigger roll-on/roll-off sequencing, and depart without human intervention.
With parcel volumes rising, conveyor lines must dynamically route products based on real-time barcode scanning. Our ODM engineering capabilities encompass modular 24V/48V electric steerable wheel diverters and 30°/45°/90° pneumatic pop-up roller transfer cassettes. Capable of sorting at speeds exceeding 90 to 120 units per minute, these units eliminate costly hydraulic hoses and provide whisper-quiet operation suitable for noise-regulated work environments.
Whether you require a standard 20-meter gravity assembly spur or a multi-zone zero-pressure accumulation system for an automated distribution center, our engineering group provides complimentary layout consultation, 3D CAD models, and rapid prototype turnarounds.
Contact UsBelow are authoritative, engineering-grade answers to the technical, operational, and commercial questions most frequently raised by plant managers, logistics directors, and industrial procurement professionals:
The universal engineering rule of thumb for stable conveyor travel is that a minimum of three rollers must be beneath the shortest rigid payload at all times (Roller Pitch = Minimum Product Length / 3). For flexible payloads, corrugated boxes with bottom sag, or heavy wire baskets like our 304 Stainless Steel Wire Mesh Baskets, we recommend a minimum of four to five rollers underneath to avoid "washboarding" and drive motor overload.
MDR technology is superior when your process demands Zero Pressure Accumulation (ZPA), energy efficiency, and low acoustic noise. In applications where products must queue without colliding (e.g., delicate electronics, carton packaging lines, or glass bottles), MDR allows each zone to stop individually. Conversely, if you are continuously moving uniform 1,500kg engine blocks across a foundry without need for queuing, a single continuous AC gearmotor with Chain Driven Live Rollers (CDLR) offers a more cost-effective mechanical solution.
For standard light carton conveyors (<30 kg), a ø50mm tube with a 1.5mm carbon steel wall and an 11mm hexagonal spring-loaded shaft is standard. For pallet handling (500 kg to 2,000 kg per pallet), our factory specifies ø76mm or ø89mm tubes with 3.0mm to 4.5mm wall thicknesses mounted on solid 20mm round shafts with milled flats or pinned axles, supported by high-load welded cast housing bearings.
Yes. That is a hallmark of our engineering capability. We frequently mount powered or gravity roller conveyor beds directly onto electro-hydraulic lift tables—such as our 3000kgs Stationary Scissor Lifter Table—to provide dynamic vertical elevation changes between mezzanine levels and ground intake docks. We also integrate infeed/outfeed gravity lanes into heavy-duty racking uprights.
In an OEM (Original Equipment Manufacturer) agreement, you supply the detailed mechanical CAD drawings, electrical schematics, and bill of materials (BOM), and our factory executes precision contract fabrication, laser cutting, welding, assembly, and testing. In an ODM (Original Design Manufacturer) arrangement, you provide system performance parameters (payload weights, facility dimensions, desired throughput rates, and electrical standards), and our in-house engineering team designs the entire mechanical and automation blueprint from scratch, validates it with FEA simulation, and manufactures the turnkey system.
Every single production batch undergoes standardized quality verification: 1) Ultrasonic tube wall thickness and concentricity run-out checks; 2) Dynamic rotational resistance and sound decibel metering; 3) Full-load continuous 48-hour endurance burn-in before crating; and 4) Remote or in-person Factory Acceptance Tests (FAT) where clients inspect live video feeds of the assembled conveyor line handling simulated test cargo.
We provide multiple protective coatings depending on environmental severity: hot-dip galvanizing (HDG) for outdoor or high-humidity ports; electrolytic zinc plating with trivalent passivation (RoHS compliant); high-durability electrostatic thermoset polyester powder coating (80–120 μm thickness) in any custom RAL color; and complete fabrication from AISI 304 or AISI 316 stainless steel for chemical, cold storage (–30°C), or pharmaceutical cleanrooms.
All roller conveyor machinery and structural storage equipment engineered by our facilities comply strictly with global safety and operational benchmarks:
Our multidisciplinary installation engineering teams deliver turnkey site layout, precise laser anchoring, electrical commissioning, and annual structural recertifications across the UAE (Sharjah, Dubai, Abu Dhabi, Ajman, RAK, Fujairah, UAQ) and export worldwide to the Americas, Europe, Southeast Asia, and the Middle East.
Initiate your factory-direct OEM/ODM roller conveyor inquiry today. Receive rapid CAD conceptual designs, customized payload stress simulations, and competitive manufacturing quotations within 24 hours.