Explore our certified heavy-duty storage, modular roll security units, and logistics platforms designed to streamline supply chains across Durban, Johannesburg, and Cape Town.
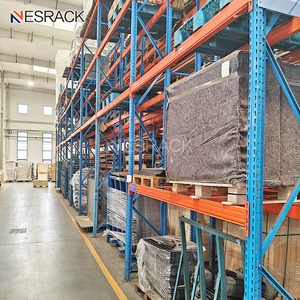
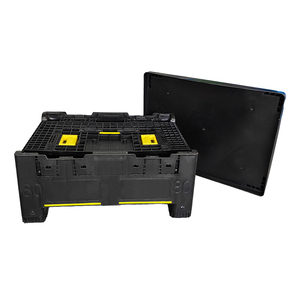
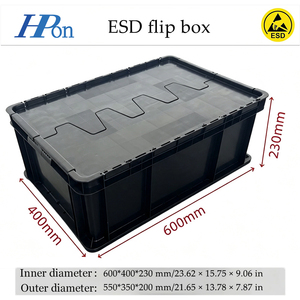
In modern industrial supply chains, an industrial roll cage container is far more than a simple wire trolley; it functions as an essential, high-turnover unit load device (ULD). As prominent manufacturers and global exporters catering to the South African industrial sector, our units are fabricated using high-yield Q235 and high-tensile cold-drawn micro-alloyed carbon steel wire. Welded at every nodal cross-section using fully automated multi-spot resistance projection welding, our cages achieve structural integrity capable of absorbing dynamic lateral shock loads during long-haul freight transport along the N3 logistics corridor between Gauteng and Durban.
Corrosion mitigation remains paramount across South Africa's diverse climates—ranging from the high-salinity coastal atmosphere of Durban Harbour to the dry, abrasive conditions of the Highveld. Every cage chassis is subjected to rigorous surface pre-treatment followed by either hot-dip galvanizing complying with SANS 121 / ISO 1461 parameters or an electro-zinc flash passivation sealed with high-molecular thermoset electrostatic powder coating. This dual barrier eliminates subterranean zinc oxidation, extending the operating life to over 10 years even under constant chemical wash-downs within pharmaceutical cleanrooms and meat-processing distribution facilities.
Kinematic versatility is achieved through precision-engineered "A-frame" nesting bases and demountable H-frame configurations. When empty, nested roll cages yield a space-saving return ratio of up to 4:1 inside intermodal trailers, drastically cutting reverse logistics freight tariffs. Integrated 125mm low-rolling-resistance elastic polyurethane (PU) and noise-dampening virgin polyamide (nylon) casters paired with precision double ball-bearing swivel heads allow warehouse pickers to effortlessly maneuver dynamic loads of up to 650kg across concrete expansion joints without operator strain.
Custom engineering deployed to eliminate touchpoints, mitigate shrink, and ensure structural compliance in Southern Africa's prime commercial clusters.
South African retail leaders operating extensive hub-and-spoke distribution networks leverage our 4-sided nesting roll cages for continuous stock replenishment directly from distribution centers (DCs) to supermarket aisles. Eliminating wooden pallets and secondary plastic wrap handling speeds up turnaround times at urban loading bays in Johannesburg and Pretoria by over 38%.
Cargo shrink during multi-drop road transit remains a primary concern for local freight operators. Our fully enclosed security roll cages feature 50x50mm high-density anti-cut steel mesh infills, tamper-evident integrated locking bars, and recessed RFID asset tracking cradles, securing electronics, cosmetics, and liquor along transit routes connecting City Deep to surrounding regional hubs.
Within temperature-controlled healthcare distribution facilities in Midrand and the Western Cape, handling protocols require non-corrosive, cleanroom-compatible equipment. Our electro-polished and hot-dip galvanized roll containers operate dependably at sub-zero temperatures down to -30°C without metal embrittlement or castor bearing seizure, maintaining cold chain integrity throughout final delivery runs.
How automation, ESG initiatives, and cross-border intra-African trade are driving demand for standardized roll logistics equipment.
Escalating regional fuel costs and congested urban retail centers are pushing logistics operators away from standard timber pallets. Roll cages allow rapid decoupling of inventory, enabling dynamic delivery trucks to load and unload goods via hydraulic tail-lifts without requiring expensive dedicated forklift infrastructures at receiving storefronts.
Modern distribution complexes across Gauteng are deploying autonomous mobile robots and AGV tow tuggers. To facilitate this automation shift, our industrial roll cages are built with reinforced towing hitch bars, directional castor pin locks, and precise dimensional tolerances, ensuring seamless integration into continuous automated transport loops.
Under the African Continental Free Trade Area (AfCFTA), cross-border freight movements into Namibia, Botswana, Zimbabwe, and Mozambique require durable, low-maintenance transport hardware. Demountable roll cages significantly maximize return payload capacity, reducing return transport costs across international freight routes.
Refined over 18 years of specialized manufacturing experience, our production lines blend advanced robotics with comprehensive quality assurance.
Every roll cage design undergoes thorough Finite Element Analysis (FEA) to verify load-bearing parameters, flex points, and weld fatigue life, tailoring dimensions to client truck configurations and facility clearances.
Our proprietary Project Tracking System gives procurement managers complete transparency into raw material preparation, weld schedules, galvanizing baths, assembly inspection, and international shipping milestones.
Our dedicated structural installation and testing teams oversee comprehensive on-site deployment, floor-leveling anchoring, column safety integration, and structural validation across all industrial territories.
Manufacturing adheres strictly to ISO 9001 quality management guidelines, EN 12674 material handling standards, and South African national safety criteria, guaranteeing reliability from trial runs through scaled operations.
Direct answers addressing technical specifications, logistical parameters, and compliance inquiries for regional procurement managers.
For installations in high-corrosion coastal regions like KwaZulu-Natal and the Western Cape, we strongly advise hot-dip galvanizing to SANS 121 / ISO 1461 standards, which provides a zinc coating thickness of 65–85 microns. This metallurgical bond ensures cathodic self-healing protection against salt spray. For inland warehouses in Gauteng, electrostatic zinc electro-plating sealed with an organic polyester powder topcoat offers dependable durability alongside custom branding color-coding.
Our A-frame roll cages feature an engineered folding base and vertical side panels that nest together securely when unladen. This system achieves a 3.5:1 to 4:1 nesting ratio, meaning an intermodal 13.5-meter tautliner trailer that carries 60 loaded roll cages can return up to 220 empty nested units. This space optimization substantially lowers empty return transportation charges on long hauls along the N1 and N3 routes.
Yes. We engineer automated-compatible roll cages with tight dimensional tolerances (+/- 2.0mm), heavy-duty reinforced chassis channels, and standardized automated tow pin brackets. Integrated guidance plates and precision-balanced low-vibration castors interface smoothly with automated warehouse towing loops, robotic sorting lines, and automatic guided transfer shuttles.
For high-capacity retail warehouses, we recommend two fixed and two swivel-braked 125mm castors featuring a high-grade polyurethane (PU) tread bonded to an aluminum or cast-iron hub. The PU formulation protects warehouse floor screeds, runs quietly below 68 dB to meet occupational noise standards, and rolls smoothly over dock-leveler transitions with a full 600kg dynamic load.
Every export consignment includes comprehensive mill test certificates (EN 10204 3.1) confirming raw material chemical and mechanical composition, static and dynamic safe working load (SWL) deflection test reports, zinc plating thickness verification logs, and complete ISO 9001 batch trace records. Full customs export declarations and bill of lading documents are coordinated to streamline clearance at Durban or Cape Town ports.
Consult with our structural design engineers to configure high-durability, custom roll containers tailored to your warehouse footprint, vehicle dimensions, and distribution workflow.
Inquire Now